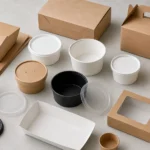
Sei pronto a creare i tuoi bicchieri di carta o le tue confezioni personalizzati con il tuo marchio?
Comunicateci le vostre esigenze — dimensioni, rivestimento, stampa e destinazione — e il nostro team vi preparerà un preventivo dettagliato entro 24 ore.
Sei pronto a creare i tuoi bicchieri di carta o le tue confezioni personalizzati con il tuo marchio?
Comunicateci le vostre esigenze — dimensioni, rivestimento, stampa e destinazione — e il nostro team vi preparerà un preventivo dettagliato entro 24 ore.
Quick Answer: How to Test Food Packaging for Leak Risk
Define your exact risk scenario first — menu item, fill temperature, fill volume, closure method, hold time, and every handling step between prep and the end customer — before you open a single sample or run a single fill.
Source and confirm the exact SKU for every component, including container body, lid, liner, and any sleeve or carrier, because a supplier revision or lot change resets your evaluation entirely.
Run representative fills using your actual menu items at your actual fill conditions and through your actual route or handoff sequence — bench tests with water alone rarely replicate the behavior of grease, sauce, or steam under real service stress.
Document every variable for every test run: menu item, fill weight, fill temperature, component lot number, closure method, hold duration, orientation, stacking conditions, and every observed result at each inspection point.
Start with the complete component set and its test variables.
Plain-English Buyer Scope
Foodservice buyers evaluating packaging for sauces, soups, steam-intensive dishes, or high-fat proteins face a recurring challenge: a container that performs acceptably in a static bench test may behave differently inside a heated holding cabinet, a stacked delivery bag, or a customer’s hands during counter handoff. This gap between catalog descriptions and real-service conditions is the focus of this guide.
This article is written for B2B foodservice purchasing teams, operations managers, and quality leads who are planning or refining a structured packaging evaluation process. The goal is a plain-English framework for defining risk scenarios, selecting components for review, running representative tests, and recording findings in a way that supports meaningful decisions across menus, routes, and service formats.
Nothing in this article constitutes a claim about the performance, food-contact suitability, or intended-use fitness of any specific Papacko SKU or any other product. All performance conclusions require exact-SKU documentation from the supplier, qualified review appropriate to your jurisdiction, and your own representative tests conducted under your actual conditions. When you explore contenitori per alimenti as part of your evaluation process, use the framework described here to structure your own assessment rather than relying on catalog descriptions alone.
Leak-Risk Variables
Before you design a test, name every variable that could contribute to a leak event in your specific operation. Buyers who skip this step tend to run generic tests that do not surface the risks that matter most to their service format.
Menu and fill characteristics. Water-based sauces, oil-based dressings, high-fat proteins, and steam-generating grain dishes each behave differently inside a closed container. The interior surface, construction geometry, and closure design of a container interact with each fill type in ways that vary substantially between menu items. For each item you plan to evaluate, document the specific fill, approximate pack temperature, fill weight or volume, and whether the fill generates condensation or internal pressure during hold.
Closure method and fit. How a lid engages the container rim — the snap geometry, the friction zone width, and the rim tolerance — determines whether pressure from steam or physical jostling can break the seal at the closure line. Evaluate every lid-and-container pairing as a matched set under your actual pack conditions, not as independent items tested separately.
Hold time and temperature environment. A container sealed at high temperature and held in a heated cabinet for forty-five minutes is under meaningfully different internal conditions than the same container handed off immediately. Define the realistic hold window for each menu item in your test matrix, including the worst-case scenario your operation actually encounters.
Route and handling sequence. Delivery routes introduce vibration, angle changes, and stacking loads that static bench tests do not replicate. Counter handoff introduces customer handling, bag-to-counter transfers, and the occasional uncontrolled drop. Each physical event is a stress event for the closure line and container walls.
Review the exact container and closure as a matched set.
Orientation and stacking. Some closure designs that perform acceptably in an upright, stable orientation show different behavior when tilted or placed under the compressive weight of other containers. If your service format involves stacking — in delivery bags, on speed rails, or in transport drawers — your test conditions must reflect that stacking geometry.
Container and Closure Review
Once you have named your risk variables, the next step is a component-level review of the exact SKUs you plan to use. This is not a visual inspection of a product photograph. It requires physical samples from the current production lot alongside the most current supplier documentation for that lot.
When you review disposable food containers with lids, request product documentation that covers rim geometry tolerances, base construction details, and any stated material properties relevant to your fill type. Read that documentation against your specific risk scenario, not as a general performance endorsement.
For each container-and-lid pairing, inspect the following:
Rim flatness and perimeter uniformity. A warped or inconsistent rim prevents a lid from engaging evenly around the full closure arc. Even a small gap at one point in that arc creates a potential liquid-migration path under internal pressure or physical stress.
Lid engagement under realistic application force. Apply the lid exactly as your staff would apply it at pack time — at the speed and hand pressure typical of your volume service flow. A lid that requires more deliberate force than your workflow allows will be inconsistently applied under real conditions, and inconsistent application produces inconsistent closure integrity.
Corner and seam construction on the container body. For containers that use folded or bonded construction, inspect corner seams under magnification when your fill type is a low-viscosity liquid or a high-fat fill that may migrate into unsealed zones. Seam construction is frequently the highest-risk location in fiber-based container bodies.
Vent or valve features. Some lid designs include small pressure-equalization features intended to manage steam buildup during hold. Understand whether those features are present on your specific SKU, where they are located on the lid, and how they affect liquid-path risk during tilt or inversion.
Liner and Construction Review
Many foodservice containers incorporate a liner, coating, or barrier layer intended to affect the substrate’s behavior when it contacts moisture, grease, or elevated heat. Understanding what is and is not documented about these layers is a critical step before any fill test begins.
Buyers evaluating coperchi per ciotole di carta or other fiber-based closures should request documentation that describes the construction layers in sequence, the material basis of any liner or coating present, and any conditions of use stated by the supplier. These supplier documents describe construction as represented by the manufacturer and do not constitute regulatory approval. They should be reviewed alongside guidance relevant to your jurisdiction and intended use.
For general framework context on how food-contact materials are categorized at a regulatory level, the FDA’s resource on food types, conditions of use, and food-contact substances provides a useful orientation — though that resource does not evaluate or approve specific commercial products, and buyers requiring regulatory conclusions for their specific use case should engage qualified regulatory counsel.
Tie every documented observation to the actual SKU.
When reviewing liner and construction documentation, pay attention to:
Stated conditions of use. Supplier documentation often describes fill temperature ranges, contact duration limits, or fill-type categories that define the scope of the stated construction. Testing outside those stated conditions produces results the documentation does not support.
Material revision tracking. Liner formulations and construction methods can change between production runs without any visible change to the external product description or catalog name. Request lot-level documentation and ask your supplier directly whether the current production lot matches the documentation you hold.
Corner and fold behavior under thermal stress. Fiber-based containers with bonded corners may respond differently at elevated fill temperatures than at ambient conditions. If your menu items involve high-temperature fills, evaluate corner and seam construction specifically at those temperatures rather than extrapolating from ambient-condition observations.
Buyers reviewing paper food boxes for high-moisture or high-fat menu items should evaluate structural integrity of the box body under saturation conditions as part of the component review stage, not only at the closure line.
Representative Buyer Testing
After component review, representative testing is where you fill containers with your actual menu items under your actual service conditions and observe behavior through the full handling and delivery sequence.
“Representative” means your actual menu item — not water, not a proxy liquid chosen for convenience — filled at your actual pack temperature, closed by your actual pack staff using their actual technique and application speed, held for your actual hold duration in your actual hold environment, and transported or handed off through your actual route or service sequence. Every substitution you make reduces the representativeness of the result and the usefulness of the finding.
Structure your test protocol around:
Multiple representative fills per condition. A single-fill observation tells you what happened once. Fill-to-fill variability in closure application force, fill level, and component geometry tolerances means that a single observation — positive or negative — is not sufficient to draw a reliable conclusion about a condition. Set the number of repetitions with your own quality reviewers according to the decision risk.
All realistic orientation and stacking conditions. If your delivery bags routinely place containers at a slight angle, test at that angle. If containers are stacked two deep under a standard delivery load, test under that compressive condition.
The full time window from pack through realistic consumption timing. If your worst-case delivery scenario is forty minutes post-pack, run tests to that full duration under those hold conditions — not to a shorter interval that feels adequate but does not match your actual service window.
Record the buyer’s own representative handling conditions.
Inspection at multiple points during the test window. Check the container exterior and any surrounding carrier lining immediately after packing, at a midpoint interval, and at the end of the test window. Note exactly where any moisture, grease migration, or liquid is first observed, and identify which component boundary it crossed.
For current SKU-level information on specific lid formats relevant to your bowl and lid pairing evaluations, the paper bowl lids product page provides a starting point for requesting documentation and samples through your account contact.
Transport and Receiving Records
Testing conducted at a prep bench does not automatically capture what happens during actual transport. Buyers who add a transport observation stage to their evaluation consistently surface failure modes that static bench tests miss.
For transport evaluation, document the vehicle type and estimated vibration profile, the bag or carrier format and container orientation within it, any temperature-maintenance equipment in use during transit, the total elapsed time from pack to delivery handoff, and the condition of each container and closure at the point of delivery before the customer opens it.
At the handoff point, photograph the container exterior, the bag or carrier lining, and the closure condition before the package is opened. These photographs and notes become your baseline for comparing subsequent route tests and for evaluating whether a reported customer complaint matches a reproducible failure mode identifiable in your test data. Records that lack this level of detail make root-cause analysis difficult and slow the process of identifying whether a problem is related to the component, the closure application, the hold condition, or the route.
Ambito editoriale e verifica degli acquirenti
This article is editorial planning guidance. It does not constitute product approval, food-contact clearance, regulatory compliance guidance, or performance certification for any Papacko product or any other packaging product.
Every conclusion about whether a specific container, lid, liner, or construction is appropriate for a specific menu item, fill condition, route, or service format requires exact-SKU supplier documentation current to the production lot in use, qualified review by persons with expertise in food-contact materials and applicable regulatory requirements, and your own representative tests conducted under your actual conditions.
Treat a changed component as a new buyer-review event.
A changed SKU — including a material revision, a construction geometry change, or a supplier source change — constitutes a new component for testing and documentation purposes, even when the product name and catalog number appear unchanged. Build this assumption into your vendor management and procurement review processes so that documentation review and testing are triggered automatically when supplier notifications or lot-change notices arrive, rather than reactively after a service incident.
Contact and Next Steps
If you are planning a packaging evaluation and want to discuss a packaging category or artwork and information requirements, contact Papacko through the website inquiry process. Keep product-suitability, performance and final documentation conclusions within your own qualified buyer review.
To begin a conversation, visit the Papacko website and use the contact form or account inquiry option. Keep your exact-SKU, menu, handling and review questions together so your internal buyer process remains traceable.
Domande frequenti
What is the single most important step to take before running any fill test?
Define your exact risk scenario in writing before you select samples or conduct any fill. That written definition should name the specific menu item, the pack temperature, the fill weight or volume, the closure method, the planned hold duration, the hold environment, and every handling step from the prep station to the customer. A risk scenario that is not defined before testing produces results that are difficult to act on because the test conditions may not reflect the actual service conditions where failure risk is highest.
Why does a changed SKU require starting the entire evaluation over?
Material properties, liner formulations, construction geometry, and seam methods can all change between production runs or supplier revisions without any visible external change to the product name or catalog number. Documentation you hold may accurately describe a previous lot but not the current one, and test results are specific to the component as it was constituted when you tested it. Any change to the component — including changes you did not initiate or observe directly — means previous test results do not apply to the current lot.
How many replicate fills are enough for a meaningful buyer test?
Run multiple representative fills per condition, with the count set by your own quality reviewers according to process variability and decision risk. A single observation showing no failure demonstrates one acceptable instance, not acceptable performance. Higher-risk menu and handling scenarios require a more deliberate review across the full test window.
Does supplier documentation from Papacko serve as food-contact or regulatory approval?
No. Supplier documentation describes construction, material composition, and stated conditions of use as represented by the manufacturer. It does not constitute regulatory approval, food-contact clearance, or compliance certification in any jurisdiction. Buyers who need regulatory conclusions specific to their use case, menu items, and jurisdiction should engage qualified regulatory counsel and conduct exact-SKU review and representative testing appropriate to their circumstances.
What records should be kept from each representative fill test run?
For each individual test run, record the menu item name, fill weight, fill temperature, every component SKU and its lot number, the closure method and any notes on how it was applied, the hold duration and hold environment, the transport or handling sequence performed, the orientation and any stacking load during transport, the elapsed time between pack and each inspection point, and every observation at each inspection point. This level of documentation makes findings traceable, allows meaningful comparison between runs, and supports root-cause analysis if a failure mode appears during evaluation or after service rollout.
How should a buyer respond when a supplier notifies them of a liner or material change?
Treat every supplier material-change notification as a documentation and testing trigger. When you receive notice of a change — or when a new lot arrives and you cannot confirm it matches your existing documentation — pause use of that lot for unevaluated menu items, request updated documentation from your supplier contact, and complete a new round of representative tests before returning to standard service use. Building this review step into your receiving and procurement procedures ensures it happens systematically rather than only after a customer report or service incident prompts a reactive investigation.
krad lin
Papacko Content Team — Realizziamo guide pratiche e basate sull’esperienza di fabbrica per il packaging B2B nel settore alimentare e delle bevande. Gli argomenti trattati includono la scelta di bicchieri e ciotole di carta, rivestimenti in PE/PLA/a base acquosa, conformità alle normative sul contatto con gli alimenti, stampa, controllo qualità e flussi di lavoro pronti per l’esportazione, affinché caffetterie, ristoranti, distributori e partner OEM possano crescere con una fornitura affidabile.